When industrial meat processors evaluate a meat mincer machine price, they are often looking for more than just a number; they are seeking a balance between initial capital expenditure and long-term operational yield. In high-volume production environments, the cost of the machinery is secondary to its ability to maintain protein integrity and ensure consistent texture across thousands of kilograms of product. The challenge lies in selecting a system that reduces waste while maximizing the absorption of marinades and seasonings.
The financial implications of choosing the wrong processing equipment can be severe, manifesting as poor moisture retention or increased microbial risk due to temperature spikes during mixing. For those focusing on the Pretreatment of meat products, integrating a vacuum-based system is no longer a luxury but a necessity to prevent oxidation and extend shelf life. The interplay between mechanical mixing and vacuum pressure directly affects the final product's color, juiciness, and overall market value.
This analysis examines the critical technical drivers that influence meat mincer machine price and how vacuum technology transforms raw mince into a high-value commercial product. By understanding the mechanics of protein extraction and atmospheric control, processors can make informed procurement decisions that optimize their ROI and ensure compliance with stringent food safety standards.


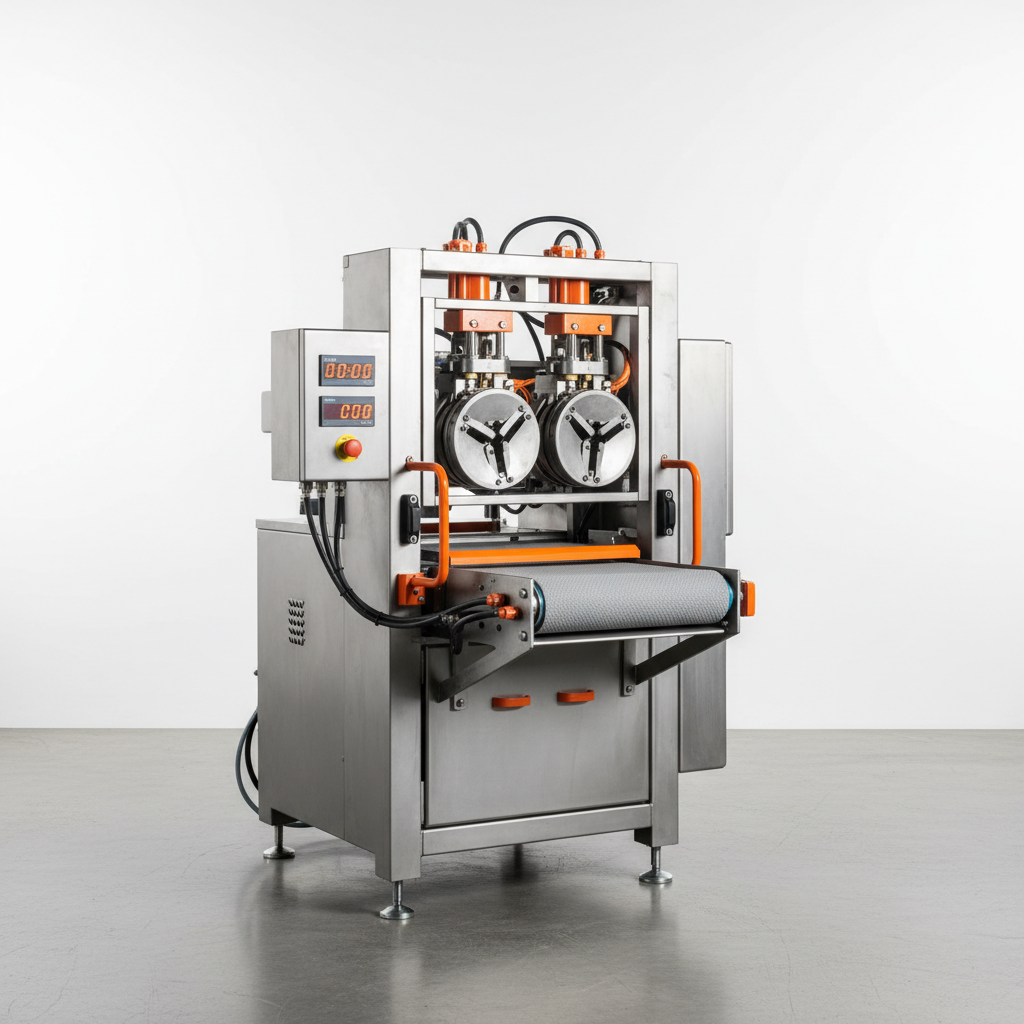
A meat vacuum mixer is a specialized piece of equipment designed to combine ingredients under negative pressure. Unlike traditional mixers, which operate in an open-air environment, these machines extract oxygen from the chamber, causing meat fibers to expand. This expansion allows brines and seasonings to penetrate deeper into the muscle tissue, significantly reducing the marination time required for large batches of sausages or hams.
The mechanical action typically involves dual-shaft mixing or tumbling, which gently massages the meat to extract myofibrillar proteins. These proteins act as a natural binder, ensuring that the final product has a cohesive texture and superior water-holding capacity. By controlling the vacuum level and rotation speed, manufacturers can precisely calibrate the consistency of the emulsion, which is critical for high-end processed meats.
The construction material is the primary driver of durability and hygiene. High-grade stainless steel is mandatory to prevent corrosion from saline injectors and cleaning chemicals. Beyond materials, the precision of the vacuum pump and the ability to switch between clockwise and counter-clockwise rotation are critical. This directional switching prevents "dead zones" in the mixer, ensuring that every kilogram of meat is treated equally, regardless of its position in the drum.
The integration of pneumatic controls for automatic cover and discharger operation reduces labor costs and minimizes the risk of contamination, making the total cost of ownership lower over a five-year lifecycle compared to manual systems.
Furthermore, capacity variations—ranging from 120kg to 2200kg per batch—influence the pricing structure. Larger models, such as those capable of handling 3000L, require more robust motors and reinforced frames to handle the immense torque and weight, which increases the initial investment but lowers the cost per unit of finished product in large-scale factories.
Vacuum processing fundamentally changes the chemical interaction between meat and additives. In a traditional environment, air pockets trapped within the meat act as barriers to seasoning. By removing these pockets, the vacuum mixer ensures a more uniform distribution of fat, spices, and brine. This prevents "spotting" in the final product and ensures that every slice of meat tastes identical.
Vacuum mixing reduces oxidation, which stabilizes the natural red color of the meat and prevents the greyish hue often seen in air-mixed products, directly increasing the retail appeal and shelf life of the end product.
Moreover, the gentle tumbling action improves protein bonding without overheating the meat. Maintaining a low temperature during mixing is essential to prevent microbial growth and avoid the breakdown of the emulsion. This temperature stability, combined with vacuum pressure, results in a higher yield by reducing moisture loss during the subsequent cooking or smoking phases.
When comparing different models of vacuum mixers, the relationship between volume and power is crucial. For instance, a model with a 150L capacity typically requires a smaller power input but offers higher agility for specialty batches. In contrast, a 3000L industrial unit requires significant power (up to 32KW) to maintain consistent rotational speed under full load.
The efficiency of the mixing process is measured by the time it takes to achieve a homogenous blend. Vacuum systems generally reduce this time by 30% to 50% compared to traditional mixers because the open fibers absorb liquids faster. This increase in throughput allows plants to process more batches per shift without expanding their physical footprint.
Vacuum mixers are indispensable in the production of high-quality sausages, cured hams, and ready-to-cook marinated meats. In a sausage production line, the vacuum mixer sits between the meat grinder and the vacuum sausage filler. By ensuring the emulsion is perfectly stable and air-free, the filler can produce casings with no unsightly air bubbles, which is a primary requirement for premium export markets.
Additionally, in the production of deli meats, these machines are used to integrate saline solutions more efficiently. The ability to customize the vacuum level allows processors to adjust the "bite" or firmness of the meat. This versatility makes the equipment suitable for both artisanal producers who require small, high-precision batches and industrial giants who prioritize massive throughput and standardization.
The industry is moving toward fully integrated "Smart Processing" cells. We are seeing a shift where vacuum mixers are linked via PLC (Programmable Logic Controllers) to the upstream grinders and downstream fillers. This ensures that the timing of the vacuum cycle is perfectly synchronized with the product flow, eliminating idling time and reducing the risk of meat sitting at room temperature.
Another emerging trend is the focus on "Cold-Chain Integration," where cooling devices are integrated directly into the mixing drum. By maintaining the meat at exactly 2-4 degrees Celsius during the high-friction mixing process, manufacturers can virtually eliminate the risk of bacterial blooms, thereby extending the naturally derived shelf life of the product without additional preservatives.
Sustainability is also playing a role, with newer designs focusing on energy-efficient motors and water-saving cleaning systems (CIP - Clean-In-Place). As environmental regulations tighten in the food sector, the value of machinery that reduces electricity consumption and chemical waste will become a primary factor in the procurement process for global food brands.
One of the primary challenges in vacuum mixing is the wear and tear on the seals. Because the machine operates under negative pressure, any leak in the gasket can lead to a loss of vacuum, which immediately impacts the marination quality. Regular inspection of the pneumatic seals and the lubrication of the rotating shafts are essential to prevent unplanned downtime during peak production seasons.
Another common issue is the accumulation of protein residue in the corners of the drum. To solve this, modern mixers utilize removable mixing arms and polished stainless steel interiors. This design facilitates rapid cleaning and prevents the buildup of biofilms, which is critical for passing HACCP and other food safety audits.
Finally, operators must be trained to balance the vacuum level with the mixing speed. Excessive vacuum combined with high speed can sometimes "over-work" the meat, leading to a mushy texture. The solution is to use variable frequency drives (VFD) to gradually ramp up the speed, ensuring a gentle yet thorough blend of fat, meat, and spices.
| Model | Capacity (Kg) | Power (KW) | Vacuum Level (Mpa) |
|---|---|---|---|
| ZJB-150 | 120 | Variable | 0 to -0.085 |
| ZJB-300 | 220 | 6 | 0 to -0.085 |
| ZJB-600 | 450 | 7 | 0 to -0.085 |
| ZJB-1200 | 900 | 12 | 0 to -0.085 |
| ZJB-2000 | 1200 | 24 | 0 to -0.085 |
| ZJB-3000 | 2200 | 32 | 0 to -0.085 |
The primary difference is the atmospheric environment. A vacuum mixer removes air from the chamber, which opens the meat fibers and allows marinades to penetrate more deeply and evenly. Traditional mixers operate in open air, which often leaves air pockets in the meat, leading to slower marination and a higher risk of oxidation and discoloration.
It increases yield by improving water and protein retention. The vacuum pressure forces the brine into the muscle fibers, while the gentle mixing extracts proteins that bind the moisture. This prevents the meat from losing excess liquid during cooking, resulting in a heavier and juicier final product.
For medium-sized operations, models like the ZJB-600 (450kg capacity) or ZJB-1200 (900kg capacity) are typically ideal. They provide a balance between high throughput and the ability to handle specialized, smaller batches without wasting energy or space.
Vacuum mixers are designed for raw, thawed mince. For frozen meat, you must use a Frozen Meat Slicer or Grinder first to reach the appropriate consistency. Once the meat is in a mince state, the vacuum mixer can be used to integrate seasonings and proteins effectively.
Maintenance involves the daily cleaning of the seal surfaces and the weekly inspection of the rubber gaskets for cracks or wear. Using food-grade lubricants on the pneumatic components and ensuring the cover is closed properly before starting the vacuum pump are critical steps to prolong seal life.
Yes, it preserves the color. By removing oxygen, the machine prevents the oxidation of myoglobin, which is the protein responsible for the red color of meat. This results in a more vibrant, natural appearance and prevents the "grey" look associated with air-exposed processed meats.
Selecting a vacuum mixing system is a strategic decision that impacts every stage of the meat production chain, from the initial pretreatment to the final retail shelf life. By focusing on the technical synergy between negative pressure and mechanical agitation, processors can achieve superior texture, color stability, and yield. The transition from traditional mixing to vacuum technology represents a shift toward a more scientific, data-driven approach to food manufacturing.
Whether you are upgrading an existing line or designing a new facility, focusing on capacity alignment and material durability will ensure long-term operational success. For those seeking customized solutions to optimize their meat processing workflow, exploring the professional range at www.ycmeatmech.com can provide the necessary technical guidance to match the right equipment with your specific production goals.